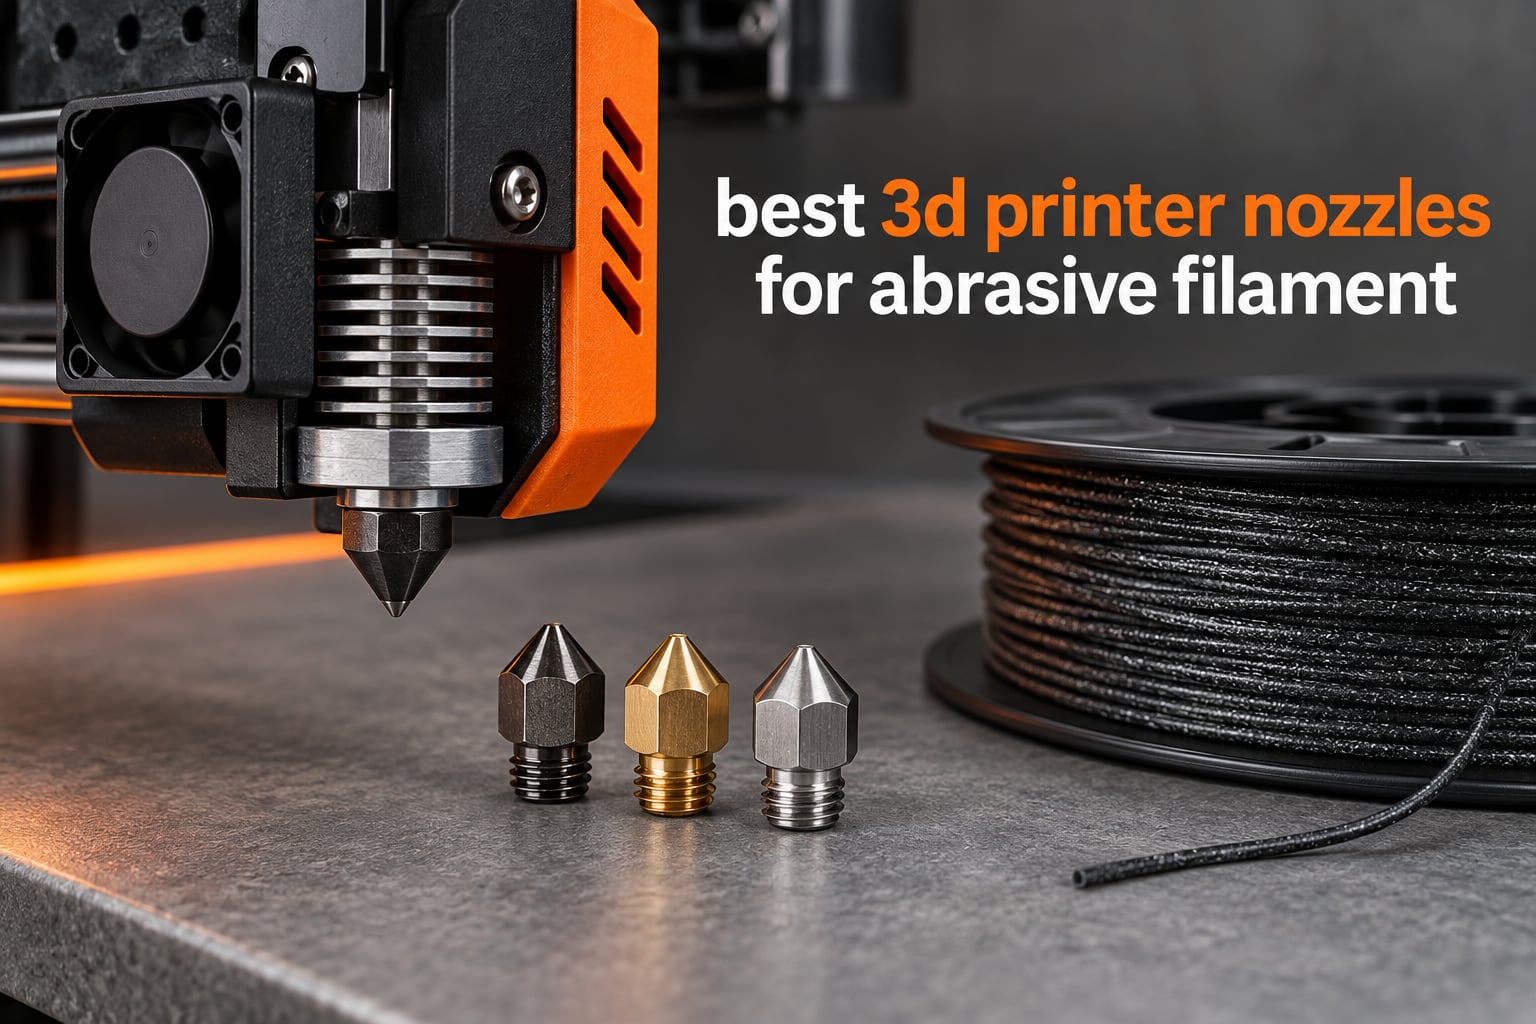
Abrasive filament does not clog a printer politely. It grinds the hole in your nozzle open, a few microns at a time, until the bore is wide and oval and your flow calibration is quietly wrong. The molten plastic itself is soft; it is the hard filler riding through the bore that does the cutting, which is why a brass nozzle that ran fine for a year of PLA can look chewed up after a single roll of carbon fiber PETG.
That is the whole problem behind this guide. We compared the best 3d printer nozzles for abrasive filament across every fitment you are likely to own, from MK8 blocks on Ender and CR-10 machines to V6 hotends and Volcano high-flow setups. Ten picks, all sourced from customer review data, each with the material, the thread, the bore sizes, and an honest note on who should skip it.
One thing up front: brass is the right nozzle for most printing, and we are not going to pretend otherwise. If you run a spool of carbon fiber twice a year, a cheap brass nozzle plus a replacement afterwards is genuinely the cheapest path. The picks below are for people who touch composites often enough that a worn bore becomes a recurring problem.
Top 3 Best 3D Printer Nozzles for Abrasive Filament (October 2026)
These three cover the most ground: the highest-volume hardened option, the highest-rated plated option, and the coated brass pick that owners report outlasting far pricier inserts.
Mudder Hardened Steel MK8 5-Pack
- Hardened tool steel
- 0.4 mm bore
- M6 MK8 fitment
- Five nozzles per pack

Micro Swiss MK8 Plated Value Pack
- TwinClad XT plating
- 0.2 to 0.8 mm orifices
- Fits CR10 and Ender MK8
Quick Picks: All 10 Abrasive Nozzles at a Glance in 2026
All ten nozzles in one view, with the material and thread that decide whether a part will even screw into your printer.
| Product | Specifications | Action |
|---|---|---|
| Mudder Hardened Steel MK8 5-Pack |
|
Check Latest Price |
 POLISI3D Hardened Steel V6 4-Size Set |
|
Check Latest Price |
| Micro Swiss MK8 Plated Value Pack |
|
Check Latest Price |
 Micro Swiss CR-10S Pro Plated 0.4 mm |
|
Check Latest Price |
| E3D Nozzle X 0.40 mm V6 |
|
Check Latest Price |
 MICREEN Hardened Steel MK8 5-Pack |
|
Check Latest Price |
 POLISI3D Volcano Hardened Steel 0.4 mm |
|
Check Latest Price |
 Dawnblade Tungsten Carbide MK8 0.4 mm |
|
Check Latest Price |
 Micro Swiss RepRap Plated 0.8 mm |
|
Check Latest Price |
 Aokin Hardened Steel MK8 5-Pack with Wrench |
|
Check Latest Price |
1. Mudder Hardened Steel MK8 5-Pack – Our Overall Pick for Abrasive Work
Mudder 5 Pcs Hardened Steel Nozzles 0.4mm Mk8 3D Printer Nozzles
Hardened tool steel
M6 thread with 0.4 mm bore
Diameter error under 0.02 mm
Five nozzles per pack
Pros
- Handles carbon fiber and glow filaments with no visible wear
- Long-term owners report no clogging or jams
- Spare nozzles on hand for quick swaps
- Clean bores confirmed on inspection gauges
Cons
- Two-flat body needs a wrench rather than a socket
- Some buyers needed temperature adjustments for heat loss
- A minority report clogging and poor extrusion
This is the nozzle with by far the largest review base in our set, and after working through that much owner feedback the pattern is consistent: it survives abrasive filament and keeps printing without intervention. The hardened tool steel carries good abrasion, heat and corrosion resistance, and the inner wall is machined smooth with a stated diameter error under 0.02 mm.
Fitment is the reason it is first. It fits MK8 hotends across Ender 2, 3, 3 Pro and 5, CR-10 all-metal, Prusa i3, Anet A8 and generic Reprap builds, so one pack covers the machines most people actually own. The listing has been live since June 2020, which is a long time for a spare part to stay relevant.
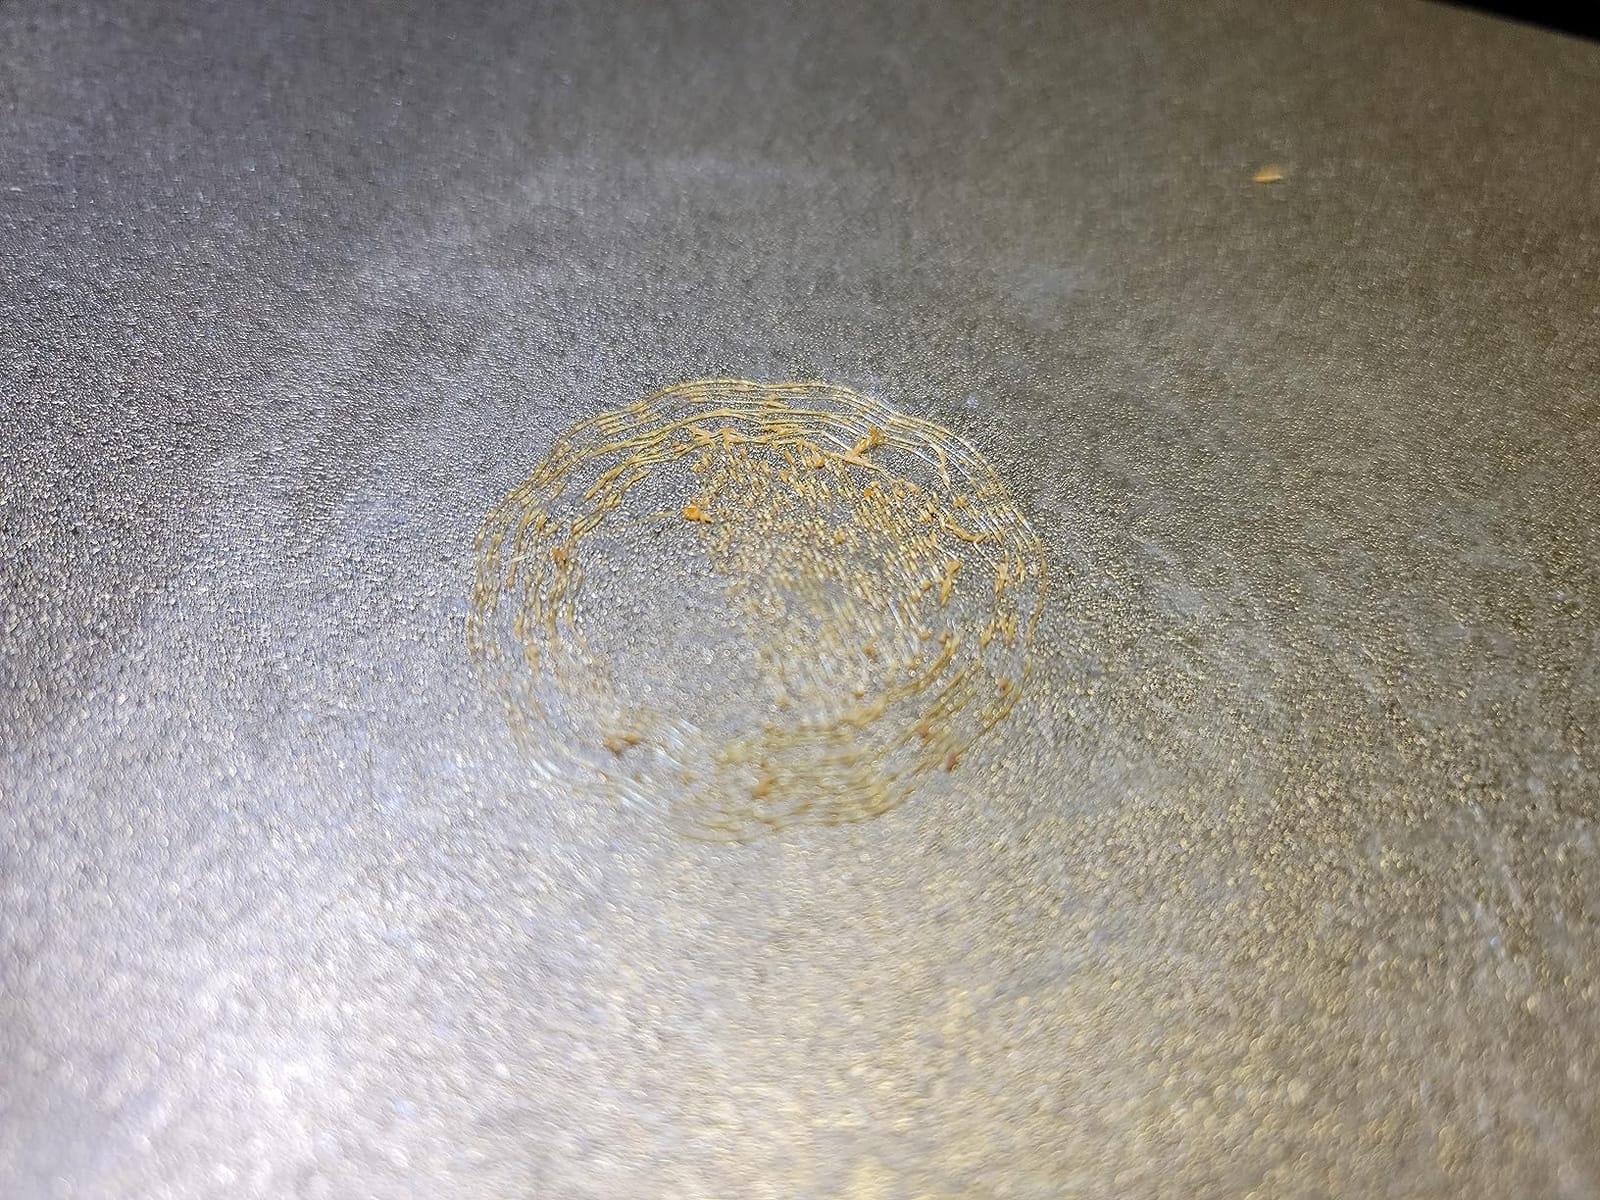
What we like most is the boring part: five nozzles in a pack means you never catch yourself running a dull bore on a spool of glow-in-the-dark. Owners running carbon-PLA blends report clean extrusion, and the orifices check out clean under magnification.
The gripes are real but small. The body is a two-flat profile rather than a full hex, so a socket will not fit and you will need a wrench. Steel loses heat faster than brass, so a temperature bump is often necessary. And a minority of reviews report clogging, which is a good reminder that budget packs vary unit to unit.
What fitment you get with this pack
Every nozzle in the pack is M6 thread with a 0.4 mm bore, sized for MK8 heat breaks. That covers Ender 2, 3, 3 Pro, 5, CR-10 all-metal, Prusa i3, Anet A8 and Reprap clones. If your hotend is a V6, this pack will not fit it and you want a V6-threaded set instead.
When to buy something else instead
Skip this if you need bores other than 0.4 mm, since all five are the same size and a mixed set is cheaper than buying twice. It is also the wrong pick for PEI and PEEK work, where a higher temperature rating matters more than pack size.
2. POLISI3D Hardened Steel V6 4-Size Set – Best Mixed-Size V6 Set
4pcs Hardened Steel Nozzles M6 Nozzle 0.25/0.4/0.5/0.6mm Compatible with 1.75mm V6 Hotend Prusa I3 MK3S Anycubic Mega S Vyper 3D Printing PEI PEEK or Carbon Fiber Filament (1×0.25+1×0.4+1×0.5+1×0.6)
CNC-machined hardened steel
0.25, 0.4, 0.5 and 0.6 mm
M6 thread for 1.75 mm V6 hotends
Pros
- Covers fine detail through fast volumetric printing in one purchase
- Outlasts brass on carbon fiber and nylon blends
- Fewer heat jams on high-flow hotends than brass
- Fits Prusa and Lulzbot V6 machines without modification
Cons
- Nozzles run slightly shorter than factory parts
- Size is marked by dots rather than printed text
- One reviewer found rust forming inside the bore
This set solves a problem the other picks do not: what to do when your abrasive prints range from a 20 mm detail part to a large bracket. You get 0.25, 0.4, 0.5 and 0.6 mm bores in hardened steel, all CNC machined, all M6 thread for 1.75 mm V6 hotends.
Owners running PEI, PEEK and carbon fiber report the steel outlasting brass, and several note fewer heat jams on high-flow hotends than they got with the original brass nozzle. Fit on Prusa i3 MK3S and Anycubic Mega S and Vyper machines is reported as clean, with no modification needed.
The main practical adjustment is Z-offset. These nozzles run a little shorter than factory parts, so you will spend a few minutes dialling in the gap after the first install. One reviewer also reported rust forming inside the bore, which points to steel that is not consistently hardened, so inspect the tip if quality matters on your project.
Marking is by dot count on the nozzle base, which is the one habit that catches people out. Learn the dot code once and the rest is easy.
Why the 0.6 mm bore earns its place
The 0.6 mm nozzle is the anti-clog option in this set, and clogging is the single most common complaint people have with fiber filaments in small bores. A wider bore also pushes more plastic per second, which matters if you are trying to finish a composite part before the weekend.
Who should skip this set
It is a V6-thread pack, so it will not fit an MK8 hotend on an Ender or CR-10. It is also not the right answer for someone who prints one material at one diameter, since a single-size hardened nozzle costs less and is simpler to track.
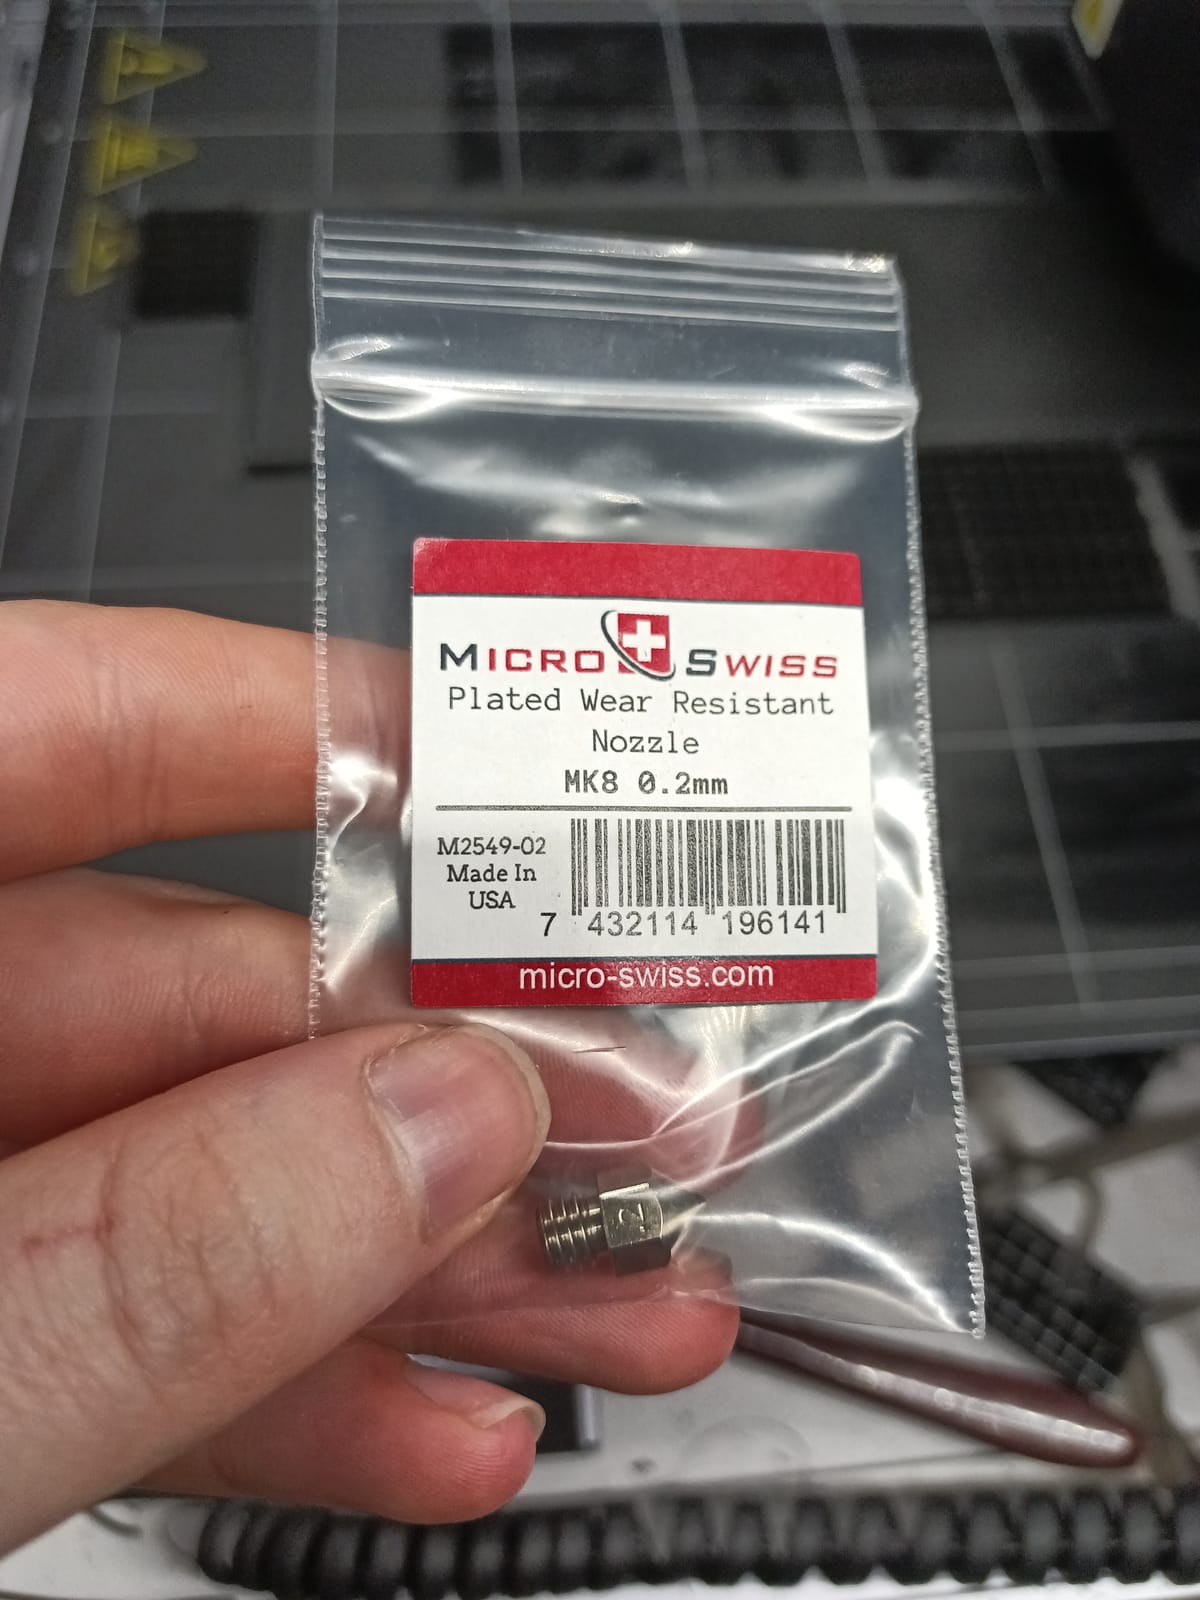
3. Micro Swiss MK8 Plated Value Pack – Highest Rated Option
Microswiss MK8 Brass Plated Wear Resistant Nozzle (MakerBot, CraftBot, Creality, CR10, Ender, Tevo Tornado) (Value Pack)
Brass body with TwinClad XT plating
0.2, 0.3, 0.4, 0.6 and 0.8 mm
Fits CR10, Ender, Tevo and MakerBot MK8
Pros
- Highest rated option in our set with 81 percent five-star reviews
- Slick coating produces noticeably smoother layer lines
- No clogging reported at any flow volume
- Repels PLA and wood-fill build-up better than plain brass
Cons
- Plating scratches if cleaned with steel wool or paper towel
- Less effective against PETG adhesion than PLA and wood
- Premium cost per nozzle versus generic steel
Micro Swiss plated brass is the name that comes up most often in community threads about Ender and MK8 builds, and this value pack is why. It is a brass body with a TwinClad XT high-lubricity wear-resistant plating, made in the USA, and it is the highest rated product in our entire list at 4.6 stars across 789 reviews.
The plating does the practical work. Owners report smoother layer lines and finer detail than off-brand brass, and they say the coating keeps PLA and wood-fill from building up on the cone the way bare brass does. Long-term users report no clogging at any flow volume, which is unusual to see reported so consistently.
What makes it attractive beyond wear is that you keep brass thermal behaviour. No temperature offset is needed, which is one less adjustment when you are already running a temperature-limited profile. The value pack spans 0.2 mm to 0.8 mm orifices, so it covers the same range as a mixed-size set without the sizing guesswork.
The failure mode is the coating itself. Scrub it with steel wool, or even a paper towel, and the plating scratches, which can produce intermittent extrusion gaps. Clean it while it is warm and wipe gently, and it will keep working.
What changes when you fit this instead of a bare brass nozzle
Very little in the slicer. Because the body is still brass, heat transfer stays close to a standard brass nozzle, so you can keep your existing temperature profile and retraction settings. That is a genuine advantage over a steel nozzle on a printer where flow is marginal.
Where the plating gives up first
PETG adhesion is the weak spot. Owners note the coating is less effective against PETG sticking than it is against PLA and wood, so expect a little more wipe-down on PETG-heavy composite prints. A few also report the smallest orifices deforming after a couple of weeks, so treat 0.2 mm and 0.3 mm as consumables.
4. Micro Swiss CR-10S Pro Plated Nozzle – Built for One Printer Family
Microswiss Plated Wear Resistant Nozzle for Creality CR-10S Pro/CR-10 MAX Original hotend ONLY (M6x.75mm Threads) (.4mm)
Brass with TwinClad XT plating
M6x0.75 thread for the original CR-10S Pro hotend
0.4 mm bore, also 0.6 and 0.8
Pros
- Solid wear resistance for carbon fiber and wood blends
- Tight manufacturing tolerances made in the USA
- Maintains dimensional accuracy over long print runs
Cons
- Restricted to the CR-10S Pro and CR-10 MAX original hotend
- Coating scratches with abrasive cleaning methods
- Fixed bore size per nozzle body
Fitment is the entire story with this one, and it is a good story if you own the right machine. The M6x0.75 thread is specific to the original Creality CR-10S Pro, CR-10S Pro V2 and CR-10 MAX hotend, which is a fitment a lot of listings get wrong.
Owners running carbon fiber and wood blends report the TwinClad XT plating holds up well, and the build tolerances are tight enough that dimensional accuracy holds over long print runs. It is made in the USA, and at 4.6 stars across 312 reviews it sits alongside the value pack at the top of our rating table.
Read the fitment line twice before you order. This one will not work on a standard V6 or MK8 hotend even though the thread size looks similar on paper, and CR-10 MAX owners have to confirm they have the original hotend rather than a later replacement assembly.
Like the other Micro Swiss parts, it is a plated brass body, so thermal behaviour stays close to a standard brass nozzle and you should not need a temperature offset. The same coating caution applies: no steel wool, no scrubbing.
How to confirm your hotend before buying
The thread on the original CR-10S Pro and CR-10 MAX hotend is M6x0.75, and the bore here is a fixed 0.4 mm with 0.6 mm and 0.8 mm variants offered separately. If you cannot confirm the hotend revision, buy a V6 or MK8 pack instead rather than gambling on a close-looking thread.
Who should skip it
Anyone on a different Creality platform, or on any Prusa, Bambu or Ultimaker machine. A plated MK8 pack is more broadly useful and costs less per nozzle, so unless you specifically own one of these three printers this is not the buy.
5. E3D Nozzle X 0.40 mm – Premium Coated Brass Pick
Genuine E3D Nozzle X – V6-1.75mm x 0.40mm (V6-NOZZLE-4TC-175-400)
Brass with a slick low-buildup coating
1.75 mm V6 0.40 mm orifice
M6 or M7 thread
Pros
- Widely reported to outlast ruby
- diamond and tungsten nozzles on abrasives
- Coating keeps filament from sticking between changes
- No temperature profile change needed versus brass
- Improves retraction and reduces stringing for some users
Cons
- Coating destroyed by paper towel cleaning
- cold pulls and steel wool
- Meant for abrasive filaments rather than plain PLA and PETG
- Costs far more than a brass nozzle
The E3D Nozzle X is the pick that makes the case for a middle tier. It is a brass nozzle with a slick coating, and it is the part number owners can reorder exactly, which matters when a coating part is something you will buy again.
Owners running carbon fiber, glass, wood and glow filament rate it very highly, with several reporting it outlasting ruby, diamond and tungsten nozzles on those materials. The coating keeps sticky and filled materials from building up on the cone, and adhered material wipes off rather than needing a hot scrape.
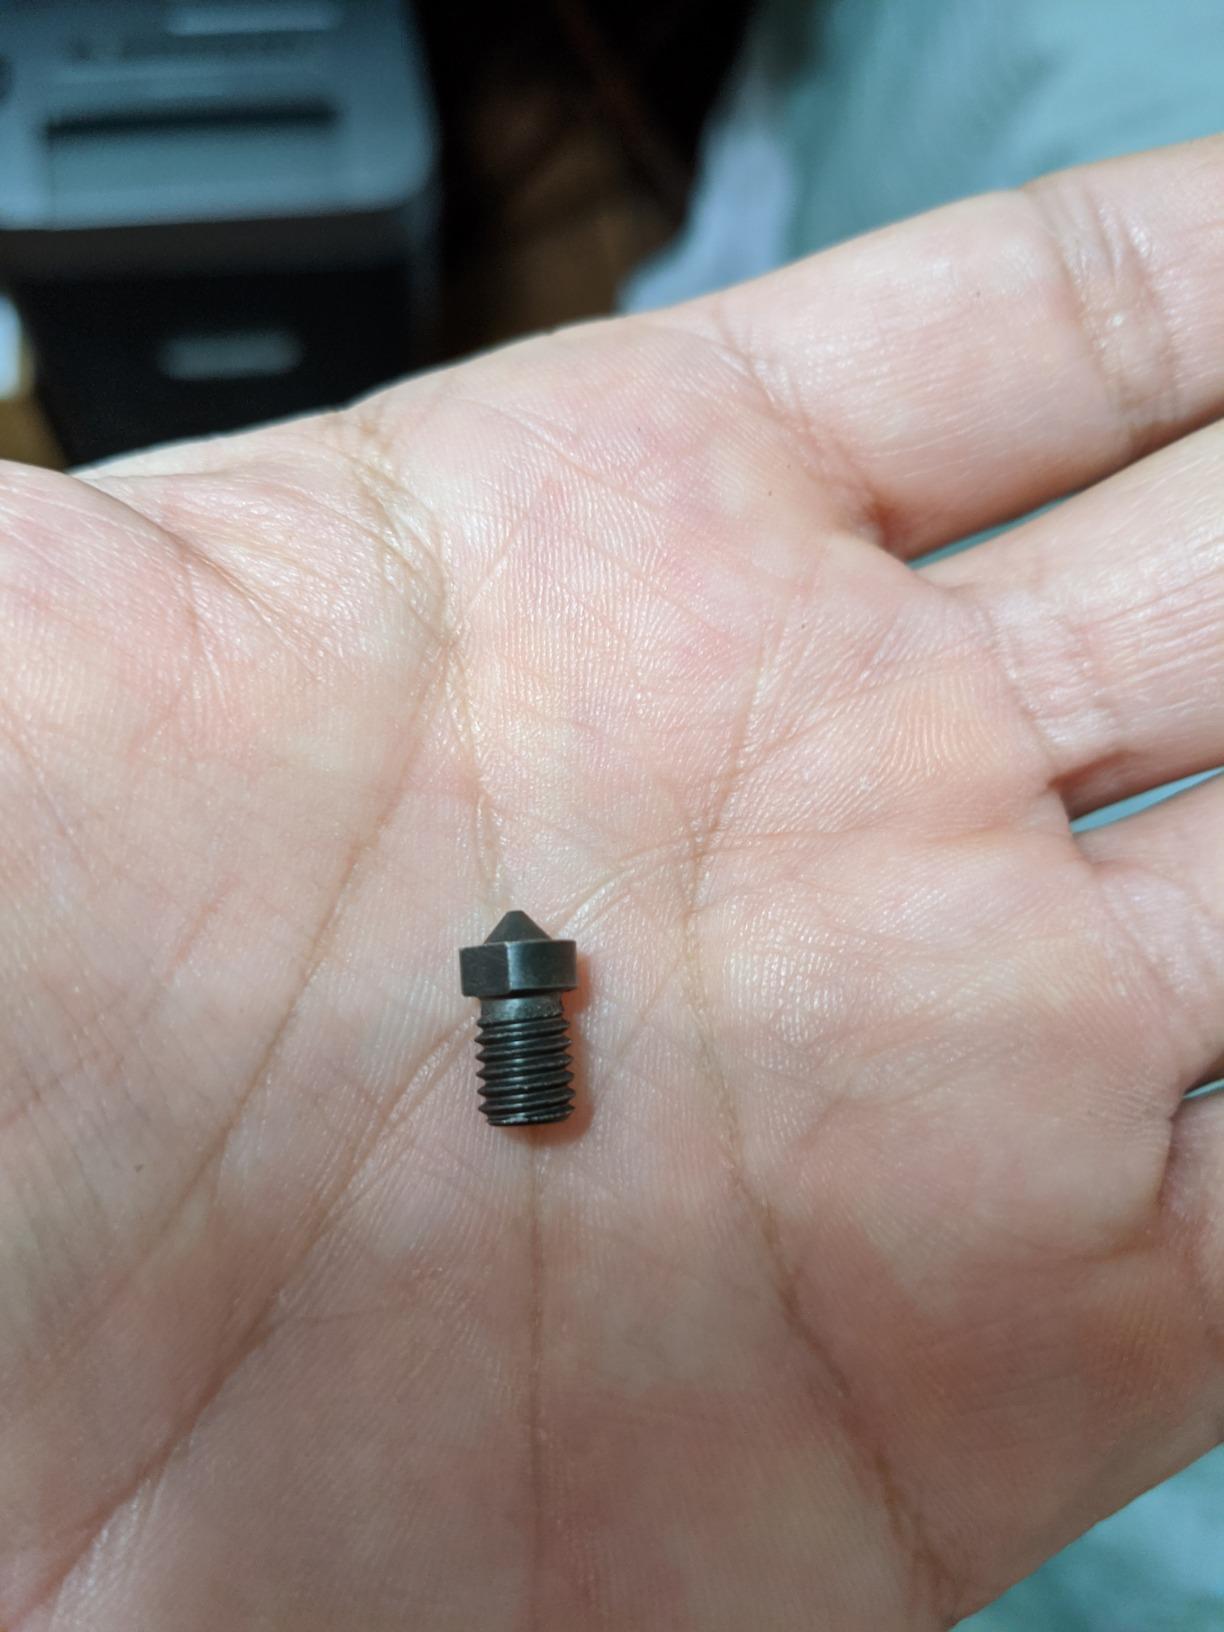
Because the body is brass, owners report no temperature profile change compared to brass on common filaments, and some see better retraction and less stringing as a side effect. It also drags less material at sharp corners, which improves first-layer reliability on composite parts that start at a sharp edge.
Two cautions. The coating is fragile against cleaning: paper towel, cold pulls and steel wool will all damage it. And it is built for abrasive material, so running it on plain PLA is spending premium money on a job bare brass handles fine.
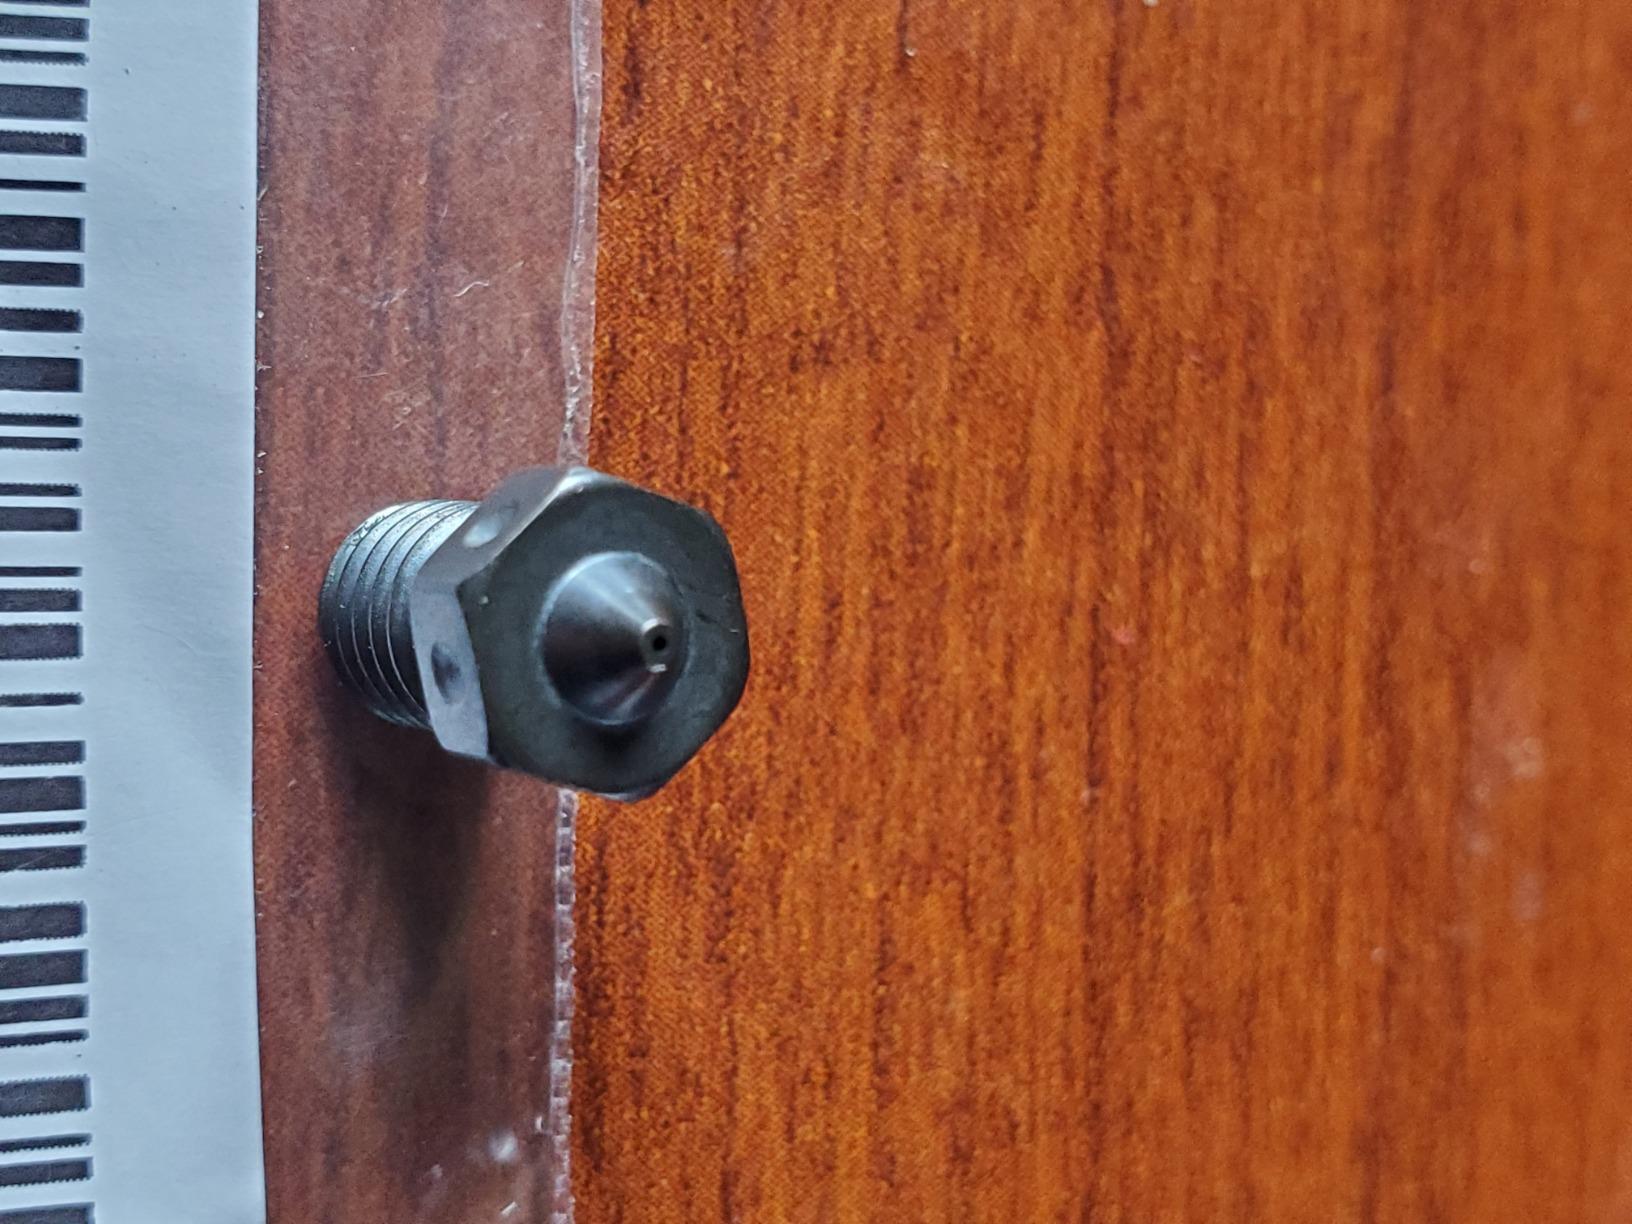
What the coated brass approach actually buys you
You keep the roughly 115 W/m·K heat transfer of brass, so there is no temperature offset to tune, and you get a surface that filled filament slides off instead of gripping. For most home printers that combination is genuinely more useful than a harder but colder nozzle.
When a harder nozzle is the better answer
If you print metal-filled filament or heavy chopped carbon in nylon, hardness eventually wins. Coated brass resists build-up and adhesion, but it is still brass, and a genuinely abrasive fill will shorten its life. In that case go up a tier to hardened steel or tungsten carbide.
6. MICREEN Hardened Steel MK8 5-Pack – The One With Published Hardness
5PCS Hardened Steel MK8 Nozzle 0.4mm Hotend Extruder All Metal Nozzle for Ender 3s 3 Pro, CR-10 3D Printer 1.75mm Filament
Hardened tool steel, 50 HRC core and 55-60 HRC surface
Rated to 450 C
0.4 mm bore, five per pack
Pros
- Publishes hardness figures at 50 HRC core and 55-60 HRC surface
- Users print carbon fiber and PEEK with it successfully
- Smooth bore gave better PETG output than the original nozzle
- Five nozzles at a low per-nozzle cost
Cons
- Thread length can be short
- leaving a gap that pulls filament and clogs
- Only one flat on the head so a special tool is needed
- Several reports of persistent clogging and failed prints
- Not compatible with Raise3D machines
Most listings just say hardened. This one states 50 HRC core with a 55 to 60 HRC surface, rated to 450 C, which is exactly the kind of number that tells you whether a steel nozzle is worth buying. It is also the only pick here that explicitly covers PEEK and PEI alongside carbon fiber.
The bore is machined burr-free at 0.4 mm, and owners report it printing carbon fiber and PEEK successfully. One user found better PETG quality than the nozzle that shipped with their Anet A8, which is a decent benchmark for a budget hotend stock nozzle.
Fitment is broad for an MK8 part: E3D V5 and V6, Ender 2, 3, 3s and 3 Pro, CR-10 all-metal, Prusa i3 and Anet A8.
Why the 450 C rating matters
Most budget hardened steel is quoted around 250 to 300 C. At 450 C this one covers PEI and PEEK profiles without the concern that the nozzle will deform mid-print, which is why it is our pick for high-temperature composite work rather than just another carbon fiber option.
The complaint to know about before you buy
Several reviews trace persistent clogging to thread length that runs short, leaving a gap where filament can be pulled and then jam, and the single-flat head means you need a purpose tool and risk a burn installing it. If clogging has already been your problem, this is not the pack to try first.
7. POLISI3D Volcano Hardened Steel Nozzle – Best for High-Flow Hotends
M6 High Temperature High Flow Hardened Steel Nozzle 0.4mm Compatible with 1.75mm 3D Printer Volcano Hotend Heat Block Sidewinder X1 X2 AC Vyper Kobra Max Print PEI PEEK Carbon Fiber (0.4mm)
Hardened tool steel
Volcano heat block M6 thread
0.4 mm for 1.75 mm filament
Pros
- No clogging and no visible wear after a full roll of glass and carbon fill
- Burr-free 0.4 mm opening confirmed on inspection
- Smooth shiny lines on TPU and finish-sensitive prints
- Works on high-flow setups printing at 100 mm/s
Cons
- Cone sits 2 to 3 mm lower than standard
- forcing Z-offset work on every swap
- Not hexagonal so an adjustable wrench is required
- Lowest average rating in the set at 4.0
Volcano hotends take a different nozzle than an MK8 block, and a lot of abrasive printing casualties come from ordering the wrong one. This is the hardened steel Volcano part, M6 thread, 0.4 mm bore, 0.6 mm and 0.8 mm variants available, with the size stamped as a number on the body.
It is listed for Sidewinder X1 and X2, Anycubic Vyper and Kobra Max, and owners report running it on high-flow setups printing at 100 mm/s. One user finished a full roll of glass and carbon filled filament with no clogging and no visible wear, and confirmed the 0.4 mm opening is burr-free under inspection.
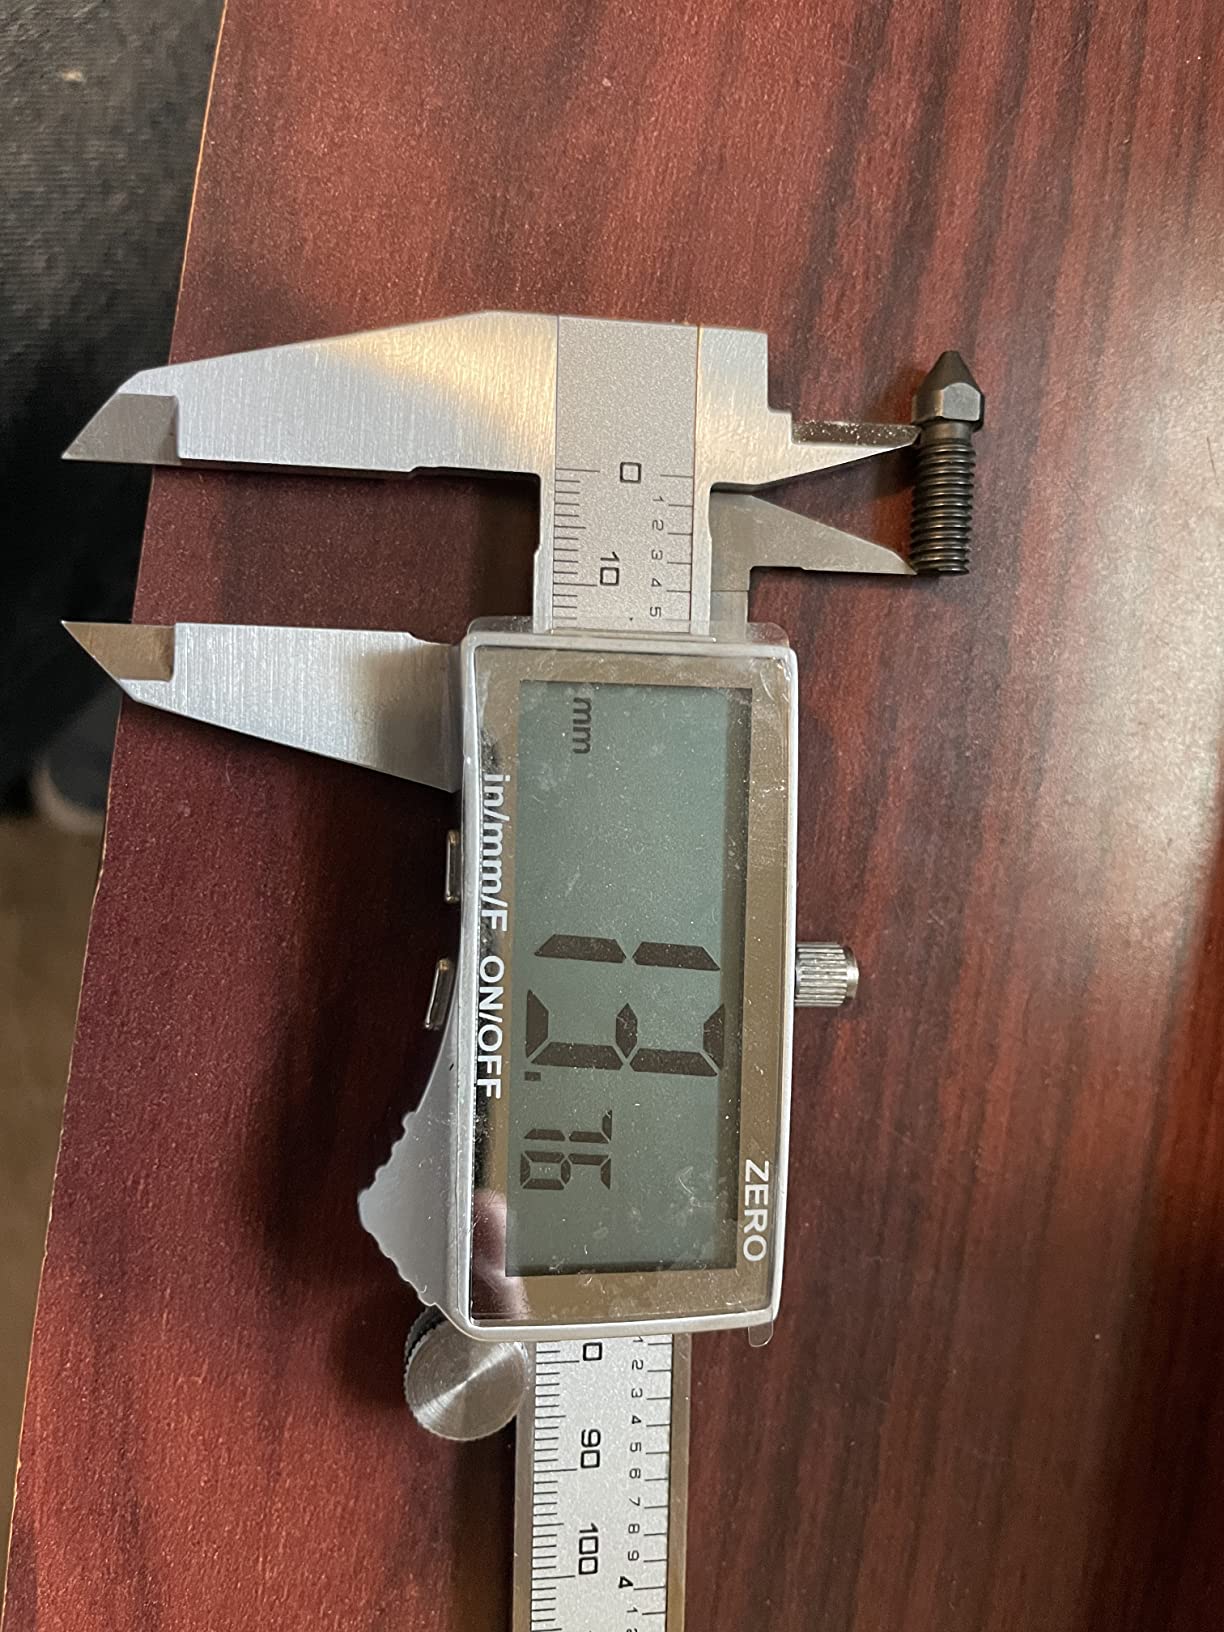
What we like is the finish. Owners report smooth, shiny extrusion lines on TPU and other finish-sensitive materials, which is not something hardened steel usually gets credit for because it is valued purely on survival.
The trade-off is installation. The cone sits 2 to 3 mm lower than a standard Volcano nozzle, so every swap means re-running Z-offset and re-levelling the bed. It is also not hexagonal, so an adjustable wrench is required. At 4.0 stars across 216 reviews it is the lowest rated product in our set, and the reviews reflect that split experience.
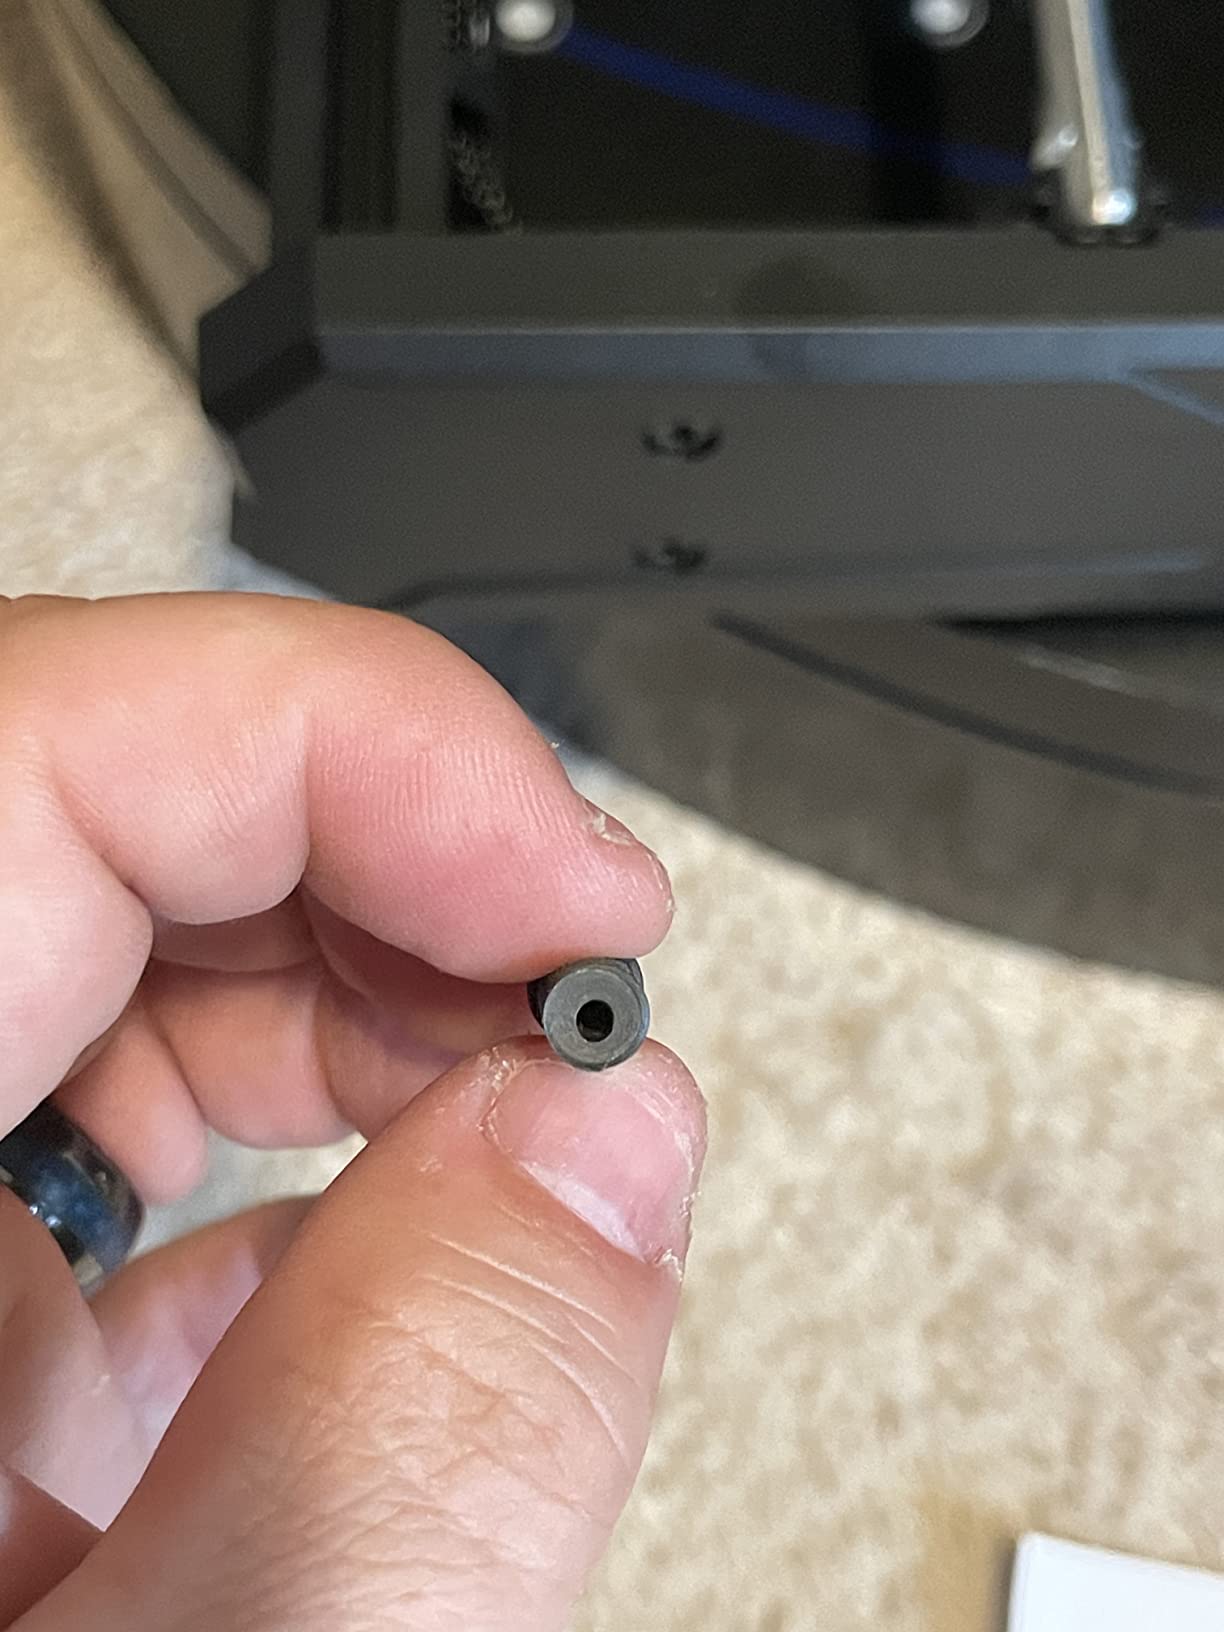
Whether you actually need a Volcano nozzle
If your hotend is a Volcano block, you have no choice in the seat and thread, so this pack removes the guesswork. If you are unsure, check your heater block shape: a Volcano-style block has a distinct wide, short heat break and a matching cone profile that sits lower than a V6 or MK8 nozzle.
Who should skip it
Skip it if your printer uses an MK8 or V6 hotend, and skip it if swapping nozzles regularly is part of your workflow, because the 2 to 3 mm cone difference means a Z-offset adjustment on every change. It is a single nozzle, so plan on ordering more than one.
8. Dawnblade Tungsten Carbide MK8 Nozzle – Hardest Material in the List
Tungsten Carbide MK8 Nozzle 0.4mm/1.75mm, Wear Resistant for 3D Printer
Tungsten carbide body rated 9 Mohs
130 W/m·K thermal conductivity
Rated to 550 C
M6 thread, 0.4 mm
Pros
- Hardest stated material in the set at 9 Mohs
- well above hardened steel
- Rated to 550 C for high-temperature filaments
- Low thermal expansion resists deformation on long prints
- Suited to MK8 Ender and CR-series hotends
Cons
- Smallest review base in the set at 81 reviews
- Lowest five-star share among the highly rated options
- Premium cost relative to hardened steel
Tungsten carbide is the tier people ask about and rarely buy. This Dawnblade MK8 nozzle is rated at 9 Mohs, which is corundum-class hardness and matches a ruby insert, with no insert to chip because the whole nozzle is the hard material.
The published specs back the marketing: rated to 550 C against 300 C for most coated nozzles, a thermal expansion coefficient of 4.5 um/m·C that resists deforming during long high-temperature prints, and fitment across MK8 Ender and CR-series hotends, CR-10, Prusa i3, Anet A8 and Reprap.
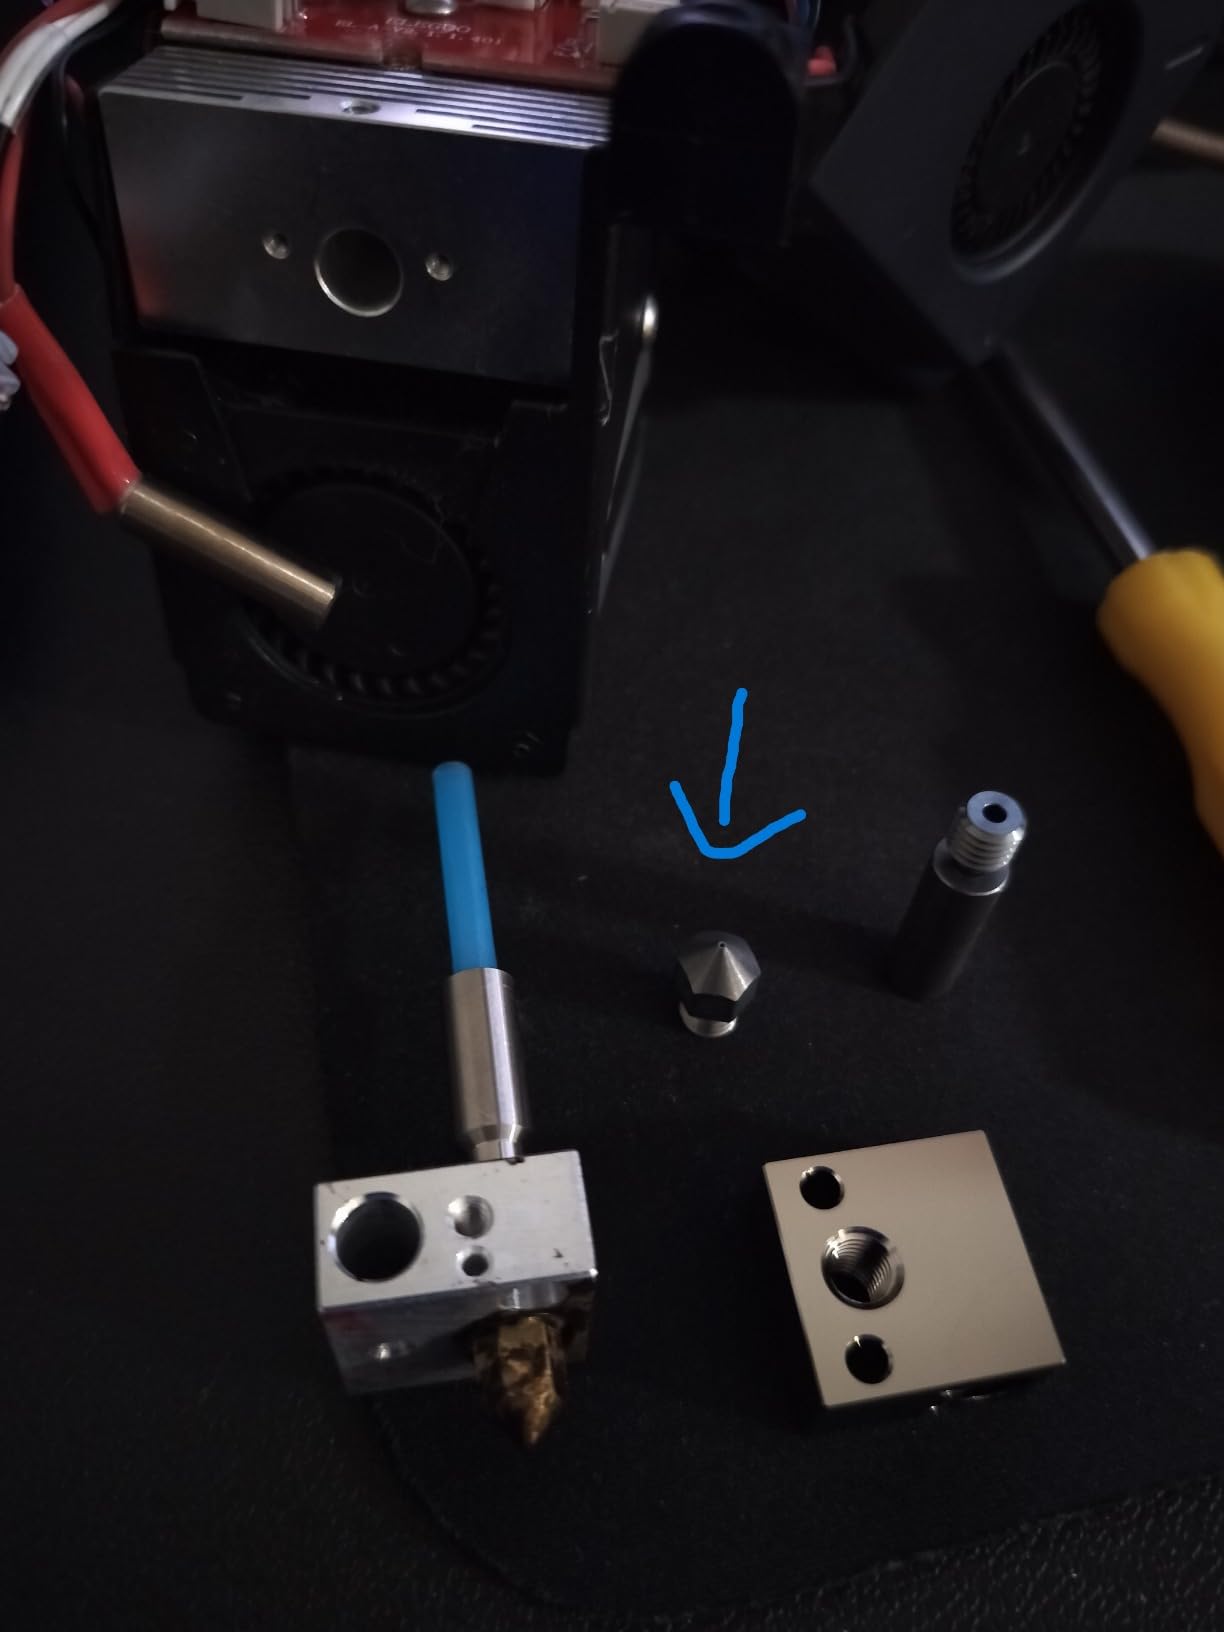
One note on the published thermal conductivity figure of 130 W/m·K. That is far above the 26 W/m·K quoted for hardened steel, and real-world behaviour of tungsten carbide nozzles is more like hard steel than like copper, so run a temperature tower before you trust a profile transferred from a brass nozzle.
The honest limitation is evidence. With 81 reviews this is the smallest customer base in our set, so there is limited long-term wear data behind the hardness claim, and its five-star share is lower than the other highly rated options. Buy it if you plan to print abrasive material continuously; do not buy it for one bracket.
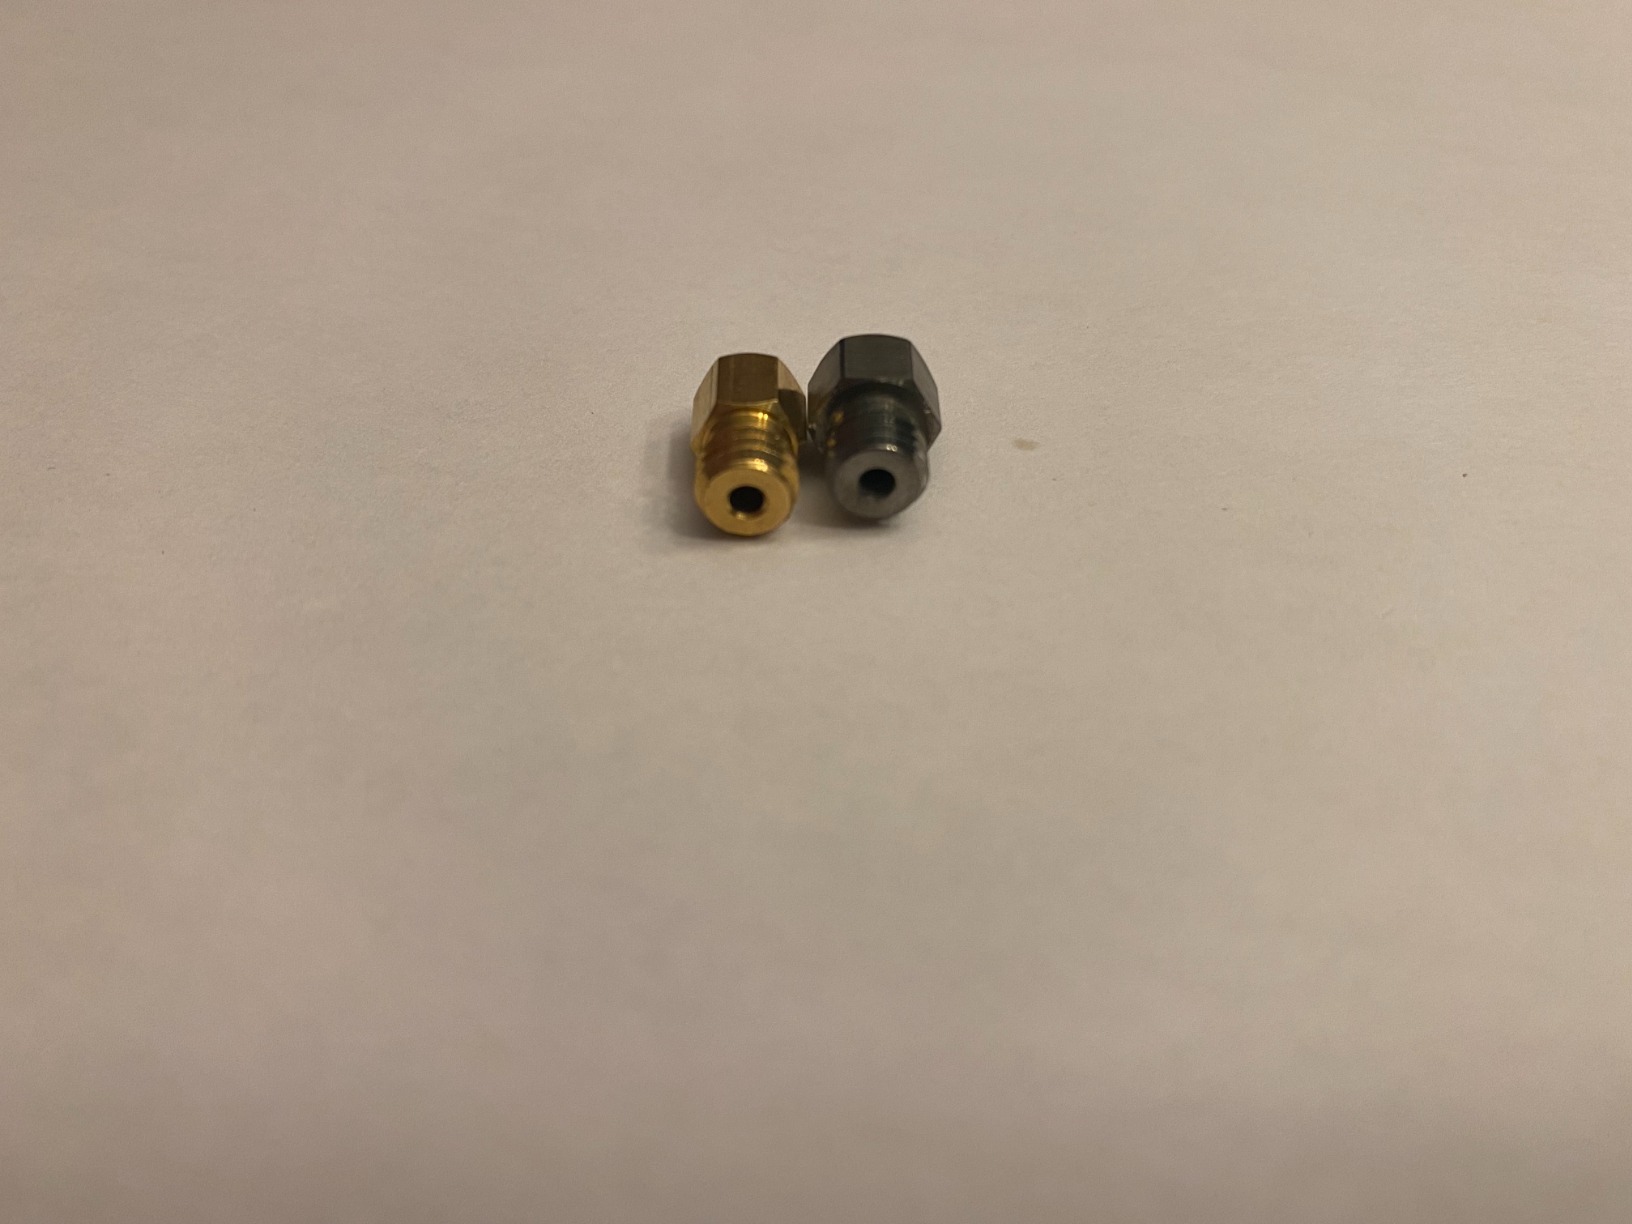
What 9 Mohs actually buys you
Hardened steel sits around 7 to 8 Mohs. Moving up to 9 Mohs is the step that changes behaviour on the most severe fills, particularly metal-filled filament and heavy chopped carbon in nylon, where a steel bore still eventually rounds off. It is the closest you can get to a ruby tip without a brazed insert that can chip.
When steel is the smarter buy
For carbon fiber PLA, carbon fiber PETG, wood fill and glow-in-the-dark, hardened steel handles it, and a five-pack of steel costs less than a single carbide nozzle. Carbide earns its price at print-farm volumes or when downtime from a clog costs more than the part.
9. Micro Swiss RepRap Plated 0.8 mm Nozzle – Built for Speed, Not Detail
Microswiss Plated Wear Resistant Nozzle RepRap – M6 Thread 1.75mm V6 Compatible .8mm
Brass with TwinClad XT plating
M6 thread, 1.75 mm V6 compatible
0.8 mm orifice for fast printing
Pros
- TwinClad coating extends nozzle life on abrasive materials
- Large 0.8 mm bore enables fast high-volume filled printing
- Also offered in 0.25
- 0.3
- 0.4 and 0.5 mm
- Consistent USA-made tolerances
Cons
- Large orifice is not suited to fine detail work
- Plating is vulnerable to abrasive cleaning methods
- Listing text still mentions a 0.4 mm nozzle on this variant
Most abrasive nozzle talk is about 0.4 mm bores, but if your goal is to get kilograms of filled filament through the machine rather than print a detailed part, bore size matters more than hardness. At 0.8 mm this nozzle moves far more plastic per second and has far less surface for a fiber to catch on.
The TwinClad XT plating still does the same job as on the smaller Micro Swiss nozzles, extending life on abrasive material, and the tolerances are consistent. Fitment is M6 thread, 1.75 mm V6 compatible, covering Prusa i3 MK2, MK2S, MK3 and Mini plus RepRap builds, and the same nozzle is offered in 0.25, 0.3, 0.4 and 0.5 mm.
How a 0.8 mm bore changes your print
Expect thicker layers, shorter print times and a rougher-looking surface, and you must change the nozzle diameter in your slicer to match. A 0.8 mm bore running against a 0.4 mm slicer profile produces heavy over-extrusion and blobs on the first layer. Set the diameter, raise your layer height ceiling, and widen your line width range to match.
Where this stops being the right nozzle
Anywhere surface finish or dimensional detail matters. A 0.8 mm bore cannot resolve a 0.2 mm feature, and finishing a large composite surface still leaves visible layer lines. Keep a 0.4 mm coated nozzle in the drawer for the parts that get looked at closely.
10. Aokin Hardened Steel MK8 5-Pack – The Cheapest Way Into Abrasive Printing
Aokin 5 Pcs 0.4mm Hardened Steel Nozzles MK8 Nozzles 3D Printer Nozzles with High Temperature Wear Resistant for Creality Ender 3/3 Pro/3 V2, Ender 5/5 Pro, CR-10/10S, Makerbot, with Flat Wrench
Five hardened steel 0.4 mm nozzles plus a flat wrench
Rated to 450 C
M6 outer thread for MK8 heat breaks
Pros
- Strong 4.6 star average with 79 percent five-star ratings
- Best sales rank in 3D Printer Extruders of this group
- Smooth bore and thread surface reduce blocking and leakage
- Flat wrench included so no special tool is needed
Cons
- Smallest review base in the set at 79 reviews
- Fitment limited to MK8-style blocks
- No bore sizes other than 0.4 mm
This is the entry point. Five hardened steel 0.4 mm MK8 nozzles, rated to 450 C, with a thin flat wrench in the box, and it holds a 4.6 star average. For anyone moving from brass to a wear-resistant nozzle for the first time, it is the lowest-risk way to find out whether a hardened bore changes anything for their prints.
Fitment is broad for an MK8 part: Ender 3, 3 Pro and 3 V2, Ender 5 and 5 Pro, CR-10 and 10S, MakerBot, Prusa i3, Tevo and Anet A8. The smooth inner wall and thread surface are designed to reduce blocking and leakage, and owners report stable temperature and even flow at higher speeds.
The included wrench solves a genuine annoyance that runs through this whole category. Several budget packs come with a single-flat head that needs a purpose tool, and installing those hot costs people time and occasionally a burn.
What you get per nozzle
Five 0.4 mm hardened steel nozzles plus a wrench, which works out to the lowest per-nozzle cost in our set. The 450 C rating covers carbon fiber and other filled filaments on a 1.75 mm PLA and ABS platform, and the M6 outer thread suits MK8 heat breaks directly.
Where it falls short
With 79 reviews the evidence base is thin, and every nozzle is 0.4 mm, so you have no high-flow option if clogging becomes a problem. It is also MK8 only. If you print a lot of composite and want options, the POLISI3D V6 four-size set or the Micro Swiss value pack give you more range for the money.
What Actually Counts as Abrasive Filament?
An abrasive filament is any filament loaded with particles hard enough to wear a nozzle bore. The molten plastic is irrelevant to the wear rate; the filler does the work.
Ranked from most to least abrasive, the order is roughly:
High-concentration chopped carbon fiber and glass fiber composites, especially chopped carbon in PETG, PA-CF and CF-PLA
Metal-filled filament, including bronze, copper and stainless steel powder loads
Glow-in-the-dark PLA loaded with phosphorescent strontium aluminate
Wood-fill and cork-fill PLA
Glow-in-the-dark is the one that surprises people. Users on r/3Dprinting describe it eating through a brass nozzle remarkably fast, and one long-running thread there has someone reporting roughly 3 kg of glow-in-the-dark plus 2 kg of wood pushed through hardened steel nozzles with satisfaction. That is the volume figure people find credible, not vague hours of use.
The wear mechanism matters because it changes what you look for. Abrasive particles act like sandpaper on the bore walls, the bore widens, it loses circularity, and the line width your slicer asks for stops matching what comes out. Published tests put a 0.4 mm brass bore at 0.52 mm after only 500 g of CF-PETG, while hardened steel showed no measurable change over 2 kg of the same filament.
The Five Nozzle Material Tiers Explained
Five material tiers show up in this niche, and the useful ranking is by hardness against the abrasive filler, not by price.
Brass, the default that works for most printing
Free-machining brass conducts heat at roughly 115 W/m·K, the best thermal transfer of any common nozzle material. It is soft, it wears fast on composites, and it is still the correct answer for PLA, PETG and ABS. Changing to a harder nozzle is a cost, not an upgrade, if you do not print fillers. If ABS is where your problems start, an enclosure that controls warping will help more than a harder bore.
Coated brass, the underrated middle tier
TwinClad XT and similar low-buildup platings sit on a brass body, so you keep brass heat transfer while the slick outer layer resists sticking. Several owners of the E3D Nozzle X report it outlasting ruby, diamond and tungsten nozzles on abrasive filament. The catch: any coating is destroyed by steel wool, cold pulls, or scrubbing with a paper towel.
Hardened steel, the practical sweet spot
Tool steel at 50 to 60 HRC runs about 25 to 30 W/m·K, roughly a quarter of brass. You will usually need 5 to 10 degrees more nozzle temperature, and users report sluggish response on dynamic flow printers. In exchange you get a bore that stays put through multiple kilograms of carbon and glass fiber, which is exactly the trade most composite printers should take.
Tungsten carbide, the hardest common material
Tungsten carbide sits at about 9 Mohs, matching corundum-class ruby, and the whole nozzle is the hard material, so there is no insert to chip. It runs to 550 C and, per the Dawnblade published figures, conducts heat at 130 W/m·K against 26 W/m·K for hardened steel. That published number is generous compared to what most users experience in practice, so plan on a temperature tower anyway.
Diamond tips, the top tier and the easiest to skip
Polycrystalline diamond inserts are the hardest option and the priciest by an order of magnitude. None of the ten nozzles below is a diamond-tip part, and for almost every home printer that is the correct call. This tier makes sense for print farms running continuous composite production, not for someone printing a bracket.
Thread and Hotend Fitment Guide: V6 vs MK8 vs MK10
Will it fit my printer is the single most repeated question in 3D printing nozzle threads, and it is the most common buyer regret. Nearly every failed nozzle purchase traced in the community comes down to a thread standard that looked right in a photo.
The thirty-second version: unscrew your current nozzle, measure the thread diameter, and check the seat. Roughly 6 mm with a 0.75 pitch means M6, which covers most V6, MK8, MK10, Volcano and RepRap machines. What differs is not the thread size so much as the hex flats, the seat diameter, and which heat block the nozzle bottoms out on.
V6: M6 thread, fits the smaller V6 heat break on E3D V6, Prusa i3, Lulzbot, Anycubic Mega S and Vyper, and many clones
MK8: M6 thread with a wider seat, fits Ender, CR-10, Prusa i3 clones, Anet A8, Tevo and MakerBot MK8 hotends
MK10: a larger thread and seat built for more melt-zone capacity and higher flow, and not interchangeable with MK8
Volcano: M6 thread on a heat block with a distinctly lower cone position, so a V6 or MK8 nozzle will not seat correctly
RepRap and generic: usually a plain M6 or M7 thread on a 1.75 mm V6-style hotend
Our picks cover all of these deliberately: five MK8 options, two V6 options, one Volcano option and one RepRap option. Before ordering anything outside this list, check the hexagon size against the wrench you already have, because a 13 mm hex on a V6 does not sit in a 16 mm wrench on an MK8.
Nozzle Diameter for Abrasive Filament: 0.4 vs 0.6 mm
For abrasive filament, 0.6 mm wins on clog resistance and throughput, and 0.4 mm only wins on surface finish and detail. That is the short answer, and the community consensus is consistent on it: fiber-filled filaments jam more often in smaller bores.
The wide bore is not just about clogging. A 0.6 mm nozzle moves more plastic per second at the same line width, which is what you want on a CoreXY or high-speed Klipper setup where you are already flow-limited. A 0.4 mm nozzle is the right call for small functional parts where dimensional accuracy matters more than print time.
There is one genuine trap, and it is not about filament width. Yes, you can use 1.75 mm filament with a 0.4 mm nozzle, because the filament input diameter and the nozzle output diameter are separate specifications and 1.75 mm is the near-universal input standard. The trap is that changing the physical nozzle means changing the slicer nozzle diameter setting. Four changes minimum: nozzle diameter, layer height ceiling, line width range, and flow and retraction recalibration.
Running a 0.6 mm nozzle while the slicer still assumes 0.4 mm causes severe over-extrusion and blob artifacts that look exactly like a hardware fault. This is the adjustment people skip and then spend an afternoon blaming their extruder for.
How to Recognize a Worn Nozzle
A worn nozzle announces itself through flow, not through appearance. The bore widens and loses circularity, so the slicer commands a 0.4 mm line and the nozzle extrudes 0.5 mm or more, and your calibration drifts even though nothing in your slicer changed.
Symptoms in the order they usually show up:
Flow calibration tests that passed months ago now fail, and re-running them does not fix it
Visible over-extrusion, rough surfaces, and parts that no longer match their sliced dimensions
First-layer squish and elephant-foot that gets worse between calibration sessions
Stringing that reappears with no settings change
Under magnification, a bore that looks oval or has burrs where it used to be round
The corrective idea is simple and it reframes the whole problem. A nozzle is not worn by the plastic moving through it; it is ground down by the hard filler it moves over. Which is why people who chase slicer settings for a month fix nothing, and why swapping back to a fresh bore of the same material instantly fixes it.
A practical check: run a 20 mm calibration cube, then inspect the bore with a loupe. If the bore measures wider than the nozzle is labelled, the nozzle is done regardless of how it looks.
How We Picked and Compared These 10 Nozzles
We compared all ten nozzles on four axes: the material and hardness it is made from, the thread and hotend it fits, the customer rating and review volume behind it, and the failure modes owners actually reported in reviews rather than the ones the listing claims to avoid.
Ratings and review counts in this guide are copied directly from customer data. We did not rank on price, because abrasive nozzles move between very different tiers and a cheap carbide nozzle and an expensive carbide nozzle are not the same purchase. Where a listing’s own claims conflict with what owners report, we went with the owners.
We also weighted fitment heavily, because a nozzle that does not screw into your heat block is not a cheaper option, it is a wasted one. That is why five of the ten picks here are MK8, the most common hotend standard in home printing.
One thing we deliberately did not do: we did not include diamond-tip or polycrystalline diamond nozzles. They exist, they are the hardest option, and for a home printer they are not the right answer. A dedicated enclosure for ABS and nylon and a good filament dryer will improve your composite results more than the top tier nozzle will.
Frequently Asked Questions
Is a 0.6 mm or 0.4 mm nozzle better for abrasive filament?
For abrasive filament specifically, 0.6 mm wins on clog resistance and throughput, because fiber-filled materials jam more often in small bores and a wider bore moves more plastic per second. A 0.4 mm nozzle wins on surface finish and detail. Either way you must change the nozzle diameter in your slicer to match the physical nozzle, along with layer height ceiling, line width range, and flow and retraction.
What is the most abrasive filament?
Ranked most to least abrasive: high-concentration chopped carbon fiber and glass fiber composites, then metal-filled filament with bronze, copper or stainless powder, then glow-in-the-dark PLA loaded with strontium aluminate, then wood-fill and cork-fill PLA. The hard filler, not the plastic, is what grinds the nozzle bore open.
What is the strongest 3D printer nozzle?
By wear hardness, tungsten carbide is the hardest common nozzle material at about 9 Mohs, with ruby and polycrystalline diamond inserts harder still. This is hardness against abrasion, not tensile strength. A stronger nozzle does not make your printed parts stronger, and it will not fix a part that was designed wrong.
Is a ruby nozzle worth it?
For most home printers, no. Hardened steel is the correct answer. Ruby is a small brazed corundum insert in a brass or steel body, and forum users repeatedly report the insert chipping rather than wearing, which is the opposite of the reliability you are paying for. Ruby only makes sense at print-farm volumes where downtime and replacement cost matter more than part cost.
What are the downsides of using hardened steel nozzles?
Hardened steel conducts heat at roughly 25 to 30 W/m·K against about 115 W/m·K for brass, so you usually need a 5 to 10 degree temperature bump and a temperature tower after switching. Users also report sluggish under-extrusion at high flow rates above roughly 20 mm³/s, especially on dynamic flow printers, and a still-wearing bore on metal-filled filament.
Why does my nozzle wear out so fast?
Because the abrasive filler is grinding the orifice, not the molten plastic. Hard particles act as sandpaper on the bore walls, the bore widens and loses circularity, and your flow calibration drifts even though no settings changed. Published testing put a 0.4 mm brass bore at 0.52 mm after only 500 g of CF-PETG, which is a 30 percent increase in diameter.
Conclusion
For most people printing carbon fiber, glass fiber, wood fill, metal fill or glow-in-the-dark on a home printer, the best 3d printer nozzles for abrasive filament come down to fitment and material, in that order. Get the thread right first, then choose the hardest material your printer’s temperature and flow can live with.
Our pick is the Mudder hardened steel MK8 five-pack, because it covers the most hotends, holds a stated bore error under 0.02 mm, and has the largest body of owner evidence behind it. If you want the highest rating and the smoothest surface finish and own an MK8 block, the Micro Swiss plated value pack is the better buy. If you are on a V6 hotend, the POLISI3D four-size hardened set covers every diameter you are likely to need.
Skip all of it if you print one spool of composite a year. A brass nozzle and a replacement afterwards costs less and takes less time. Buy a wear-resistant nozzle when the bore is a recurring problem, and run a temperature tower after you fit it. Prices and availability move, so check the current listing before you order, and we have kept this guide updated through 2026.